Technical Article
Food Screw Conveyor for Extrusion Lines: How to Select a Stable Powder Feeding System
A food screw conveyor may look like a minor auxiliary machine, but it can determine whether an extrusion line runs steadily. In snack, cereal, pet-food and aquatic-feed processing, poor powder transfer can create fluctuating feed rate, changing extruder fill, off-spec product and unplanned cleaning stops.
The practical question is not only screw diameter or motor power. It is: can the system move the actual powder blend at a stable mass rate, remain hygienic, be cleaned safely and match the line’s true production demand?
1. Where a food screw conveyor fits
Dry ingredients are normally received, weighed and mixed before they enter an extruder. A screw conveyor transfers the blend from mixer to hopper, preconditioner or the food extruder. From there, a feeder supplies the required dry mass rate to the process.
- Transfer screw: selected around distance, incline, access and cleaning.
- Volumetric feeder: delivers a nominal volume at a selected screw speed.
- Gravimetric feeder: uses weight feedback to maintain a target mass rate.
- Preconditioner feed: supplies material before water, steam or liquids are added.
Do not accept one generic line item called “screw feeder” without defining these responsibilities. A transfer conveyor that is forced to control recipe flow can create instability; a precision feeder cannot solve a poorly designed material-transfer section upstream.
2. Powder flow changes finished product quality
Food extrusion begins as powder handling. Food-powder research shows that material moves from hopper through a feeder screw and into the extruder, and that particle size, composition, cohesion and moisture affect this flow. If powder enters inconsistently, the extruder does not receive the same fill from minute to minute.
That variation can change barrel pressure, mechanical energy, residence time and melt condition. On a directly expanded snack line, the result may be uneven size, density, texture, color or breakage even when barrel-temperature settings are unchanged. On pet-food and feed lines, it can also affect pellet consistency and dryer loading.
3. Information needed before selecting the screw
- Main ingredients and blend ratio;
- Particle size range: flour, meal, starch, protein powder or premix;
- Incoming moisture, fat level and tendency to stick or cake;
- Bulk density and whether it changes after mixing or storage;
- Required minimum and maximum mass rate in kg/h;
- Length, incline, elevation change and available layout space;
- Cleaning frequency, allergen changeover and food-contact requirement.
Fine or cohesive powders can bridge above the screw, compact in the hopper or form a tunnel known as rat-holing. Blends can segregate when particles differ in size or density. These are material-system issues, so a powder sample or representative formulation is far more useful than a generic capacity request.
4. Volumetric feed versus mass-rate control
A volumetric feeder can be appropriate for a stable, free-flowing material. Its limitation is that screw RPM represents volume, not mass. If a powder compacts and bulk density rises, the same RPM delivers more kilograms to the extruder.
For fine, cohesive, high-value or recipe-sensitive blends, a gravimetric feeder should be evaluated. It measures loss of hopper weight over time and adjusts screw speed toward the selected mass rate. It does not eliminate the need for a suitable hopper and a flow test, but it reduces normal density variation reaching the extruder.
| Material situation | Typical starting point | What to test |
|---|---|---|
| Stable corn or rice flour | Transfer screw plus volumetric feed may be suitable | Bulk-density change and startup repeatability |
| Fine, cohesive or variable multigrain blend | Conditioned hopper and mass-rate control should be evaluated | Bridging, arching, refill behavior and rate stability |
| Tightly specified or costly formula | Gravimetric control is often justified | Accuracy at minimum and maximum operating rate |
5. Hopper design and bridging
If material does not enter the screw consistently, increasing screw speed is rarely the lasting solution. Hopper-wall angle, outlet geometry, powder cohesion, moisture pickup and refill practice can all be responsible. Depending on the material, a suitable agitator, bridge breaker or different outlet geometry may be needed.
Every anti-bridging device must also be evaluated for hygiene and segregation. Aggressive agitation can break fragile inclusions, separate a blend or increase cleaning time. The correct design should follow a representative material test rather than a standard drawing.
6. Match the feeding section to real production capacity
Start with the line’s required dry-feed mass rate, then include a realistic operating margin. Do not choose a screw solely from a broad kg/h claim without knowing the bulk density and filling ratio used for that claim.
Required feeder rate = target dry-feed rate + normal control margin
The transfer screw must replenish the receiving hopper without running continuously at its limit. The feeder must then maintain stable delivery for the pet-food, snack or aquatic-feed process. Mixer batch size, refill interval and operator procedure should be considered with the conveyor—not after installation.
7. Hygiene, access and safety
Food screw conveyors have moving entrapment points and product-contact surfaces. The specification should include covers, guards, interlocks where access is possible, safe cleaning access, food-contact stainless-steel scope, seals and a lockout procedure. Safety guidance for screw conveyors emphasizes isolating the screw hazard and using appropriate interlocked covers where they can be opened.
For frequent recipe changes or allergen control, agree the cleaning method, dismantling time and inspection points before purchase. A machine that can convey powder but takes too long to clean will not meet its real production schedule.
8. Include feeding in the acceptance test
The feeding section should be checked during the factory acceptance test, not treated as an accessory. Record material flow at startup, normal operation and hopper refill; timed mass delivery; bridging, leakage and dust; response to rate changes; cleaning access; and guard/interlock performance.
9. A better quotation request
Send the supplier a product photo, ingredient list, powder sample or detailed material description, target kg/h, layout dimensions, elevation changes, cleaning requirement and destination voltage. Our food machinery quotation checklist helps buyers provide the inputs needed for a practical complete-line proposal.
Technical references
- Processes: Food Powder Flow in Extrusion—Role of Particle Size and Composition
- Powder densification and screw-layering in continuous feeding
- WorkSafe guidance for screw-conveyor guarding and maintenance
Need a stable feeding section for your extrusion project?
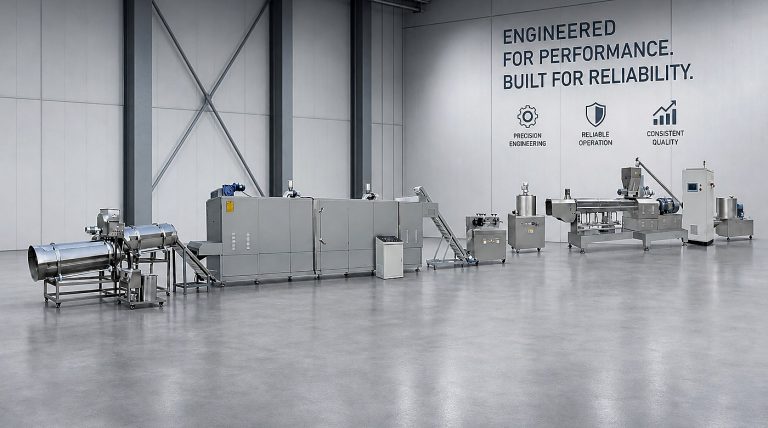
Send ZEKO your raw-material details, target kg/h, layout and cleaning requirements. We can help define the mixer, screw transfer, feeding and extrusion scope around the real product.
Continue Reading