Technical Article
Millet and Vegetable Chips: Why Microwave Puffing Starts Before the Microwave
A microwave machine is often treated as the “puffing step” in a chip project. In practice, it is rarely that simple. If the product entering the microwave has the wrong moisture, an uneven sheet thickness or a weak internal structure, more microwave power does not solve the problem. It usually makes the result less stable.
We recently discussed a 300 kg/h concept for millet-and-vegetable chips made from gelatinized millet flour blended with vegetable puree. This was a feasibility evaluation, not a delivered-line performance claim. The useful part of the discussion was not the model number of the microwave. It was the water path: reduce the formed product from roughly 45% moisture to about 15% before microwave puffing, then use gentle finishing drying to reach approximately 5–6%.
The microwave is not the first drying decision
At around 45% moisture, a formed sheet can still be soft, dense and difficult to expand consistently. Some water is needed for puffing, but too much free water can turn the microwave stage into a heavy evaporation job rather than a controlled expansion step.
That is why this route started with staged drying. The first drying section is expected to bring the sheet to a condition where the internal structure can respond to rapid heating. The microwave stage then helps create the pressure release and open texture. A low-temperature finishing section removes the remaining moisture without over-darkening the product or making the surface brittle too early.
The 15% figure is not a universal setting. It is a working target to test against the specific millet base, vegetable solids, thickness and desired bite. A thinner chip, a different puree ratio or a denser dough can move the best transfer point in either direction.
What 300 kg/h means in a moisture calculation
Capacity discussions become clearer when the moisture load is written down. Assuming the 300 kg/h figure refers to wet formed product at 45% moisture, it contains about 165 kg/h of dry solids.
- At 15% moisture, those same solids would weigh about 194 kg/h. The first drying section therefore removes roughly 106 kg of water per hour.
- At a 5.5% final-moisture target, finished production would be about 175 kg/h. The finishing section removes another roughly 19 kg of water per hour.
Those are planning figures, not a promise of final output. They do show why “300 kg/h microwave puffing line” is incomplete wording. The wet-feed basis, moisture targets, residence time and usable belt area all need to be known before equipment duty is selected.
Four points we would test before fixing the equipment
1. Sheet thickness and cut geometry
Small differences in thickness change how fast moisture moves from the center to the surface. They also change expansion and the risk of edge scorching. The trial sample should represent the intended production shape, not only a hand-made piece.
2. Moisture uniformity after the first dryer
An average reading of 15% is not enough if one side of the sheet is much wetter than the other. Uneven moisture often shows up later as mixed texture, curling or unstable puffing.
3. Microwave response and belt loading
Power density, loading depth and residence time have to be evaluated together. A good result at a lightly loaded laboratory belt does not automatically scale to a continuous industrial feed.
4. Cooling and final moisture
A chip can leave the dryer feeling crisp and still soften after packing if cooling is rushed or final moisture is not stable. The finishing stage needs to be reviewed together with cooling time and the intended package barrier.
Why the line should be discussed as one route
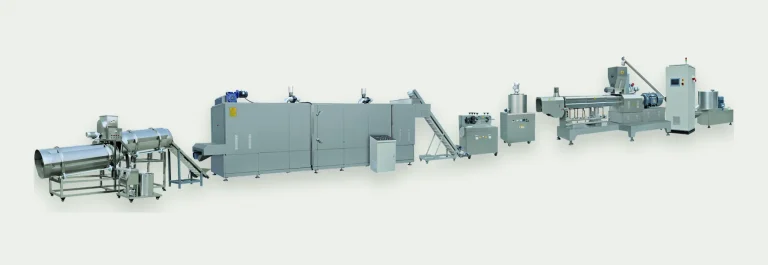
For this kind of product, the first dryer, microwave section and finishing dryer should not be quoted as three isolated machines. Their jobs overlap: one prepares the structure, one creates expansion, and one protects the final texture. A change in the first stage can reduce microwave load; a change in the microwave response can alter the final drying requirement.
That is the reason we ask for the raw-material description, target thickness, initial and final moisture, desired texture, available utilities and a representative sample before finalizing a proposal. It gives the project a better starting point than choosing equipment from a catalogue photo.
If you are evaluating microwave puffing, see our industrial microwave drying and sterilization equipment overview, or send a project brief with the material and moisture targets you are working with.
Questions buyers ask before a microwave puffing trial
Can millet-and-vegetable chips go directly into microwave puffing at 45% moisture?
Some materials may respond differently, but for the 300 kg/h feasibility concept discussed here, around 45% moisture was treated as too wet for stable continuous puffing. Pre-drying toward about 15% was used as a trial target so the microwave stage could focus on controlled expansion rather than heavy water removal.
Is 15% the correct moisture before microwave puffing for every chip?
No. The appropriate transfer moisture depends on the millet base, vegetable solids, sheet thickness, product density and required texture. It must be confirmed with representative material trials rather than copied from another product.
How should a 300 kg/h microwave puffing project be specified?
State whether 300 kg/h means wet feed or finished product, then provide initial and final moisture, product thickness, target texture, operating hours, utilities and packaging requirement. These details determine drying load, microwave residence time and the finishing section.
For a route-selection comparison, read Microwave vs Hot-Air Dryer for Food Processing. If you are preparing an inquiry, our food machinery quotation checklist shows the technical details that make an equipment discussion more useful.
Continue Reading