Technical Article
Twin-Screw vs Single-Screw Snack Extruders: A Practical Selection Guide
Choosing between a single-screw and a twin-screw food extruder is not a question of which machine is more advanced. It is a process-selection decision. The correct choice depends on the finished snack, the formulation, the way the product expands, the expected product range and the equipment around the extruder.
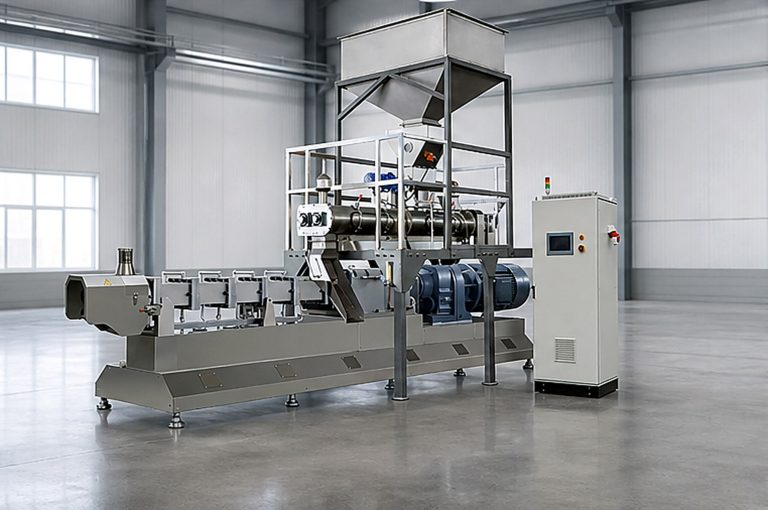
Before comparing screw arrangements, define the required product route and the role of the food extruder machine in the complete snack process. The correct choice depends on the finished product, not on the number of screws alone.
This guide is written for project owners comparing snack extrusion equipment. It explains where the two machine types differ, what those differences mean on a production floor, and what information should be fixed before asking suppliers to quote.
Start with the finished product, not the screw count
Two products can both be called puffed snacks and still require different process routes. A directly expanded corn puff, for example, develops much of its shape and texture as the cooked melt exits the die. A pellet snack can leave the extruder as a dense semi-finished piece, then expand later in a fryer. The correct extruder is part of that whole route.
Before comparing machines, define the product in physical terms: raw materials, product shape, target bulk density, moisture at packing, whether it expands at the die or later, and whether the line must run more than one family of products. Product photos and samples are more useful than a generic request for a “puff machine.”
What changes inside each extruder
Single-screw extrusion
A single-screw extruder has one screw in the barrel. It can be an effective, robust solution when the material is relatively consistent and the process window is well understood. In food extrusion, conveying and pressure development are more dependent on material friction, fill and the behavior of the formulation inside the barrel. That makes raw-material consistency, feed condition and operating discipline important.
For a stable, defined product route, a single-screw system can be practical. It is often associated with simpler forming duties and with pellet routes in which the final expansion occurs downstream. It should not be treated as a low-cost substitute for a twin-screw process when the formula, mixing demand or product range requires more control.
Twin-screw extrusion
A twin-screw extruder uses two screws that work together to convey, mix and shear the material. In food processing, intermeshing twin-screw designs can offer more positive conveying, more mixing options and more control over moisture, temperature, screw speed and screw configuration. This is especially useful when the product must expand directly at the die, when ingredients vary, or when the line must be developed around several shapes and recipes.
The added flexibility comes with a more complex machine, a larger investment and a need to specify the operating package properly. A twin-screw extruder is not automatically the correct answer just because it has two screws. The process must still have the correct preconditioner, feeding, die, cutting, drying, seasoning and controls.
When a twin-screw process is usually the stronger fit
A twin-screw snack line is normally the better starting point when the project needs one or more of the following:
- Direct expansion at the die for corn puffs, cereal rings, balls, curls or shaped cereal snacks.
- Formula changes involving different cereal flours, starch levels, inclusions or moisture targets.
- More demanding mixing and hydration before the die.
- Multiple product shapes with planned die changes.
- A development route where product samples will be refined before final acceptance.
- A defined production line rather than an isolated forming machine.
These conditions do not guarantee a particular extruder size or screw configuration. They indicate that the supplier should evaluate the product and process together instead of quoting from motor power alone.
When a single-screw route can be appropriate
A single-screw process can be appropriate when the product and formulation are stable, the process is simpler, and the project does not require the same level of mixing and recipe flexibility. For snack projects, this can include dense pellet or semi-finished products intended for later frying or a narrowly defined product range with established raw material control.
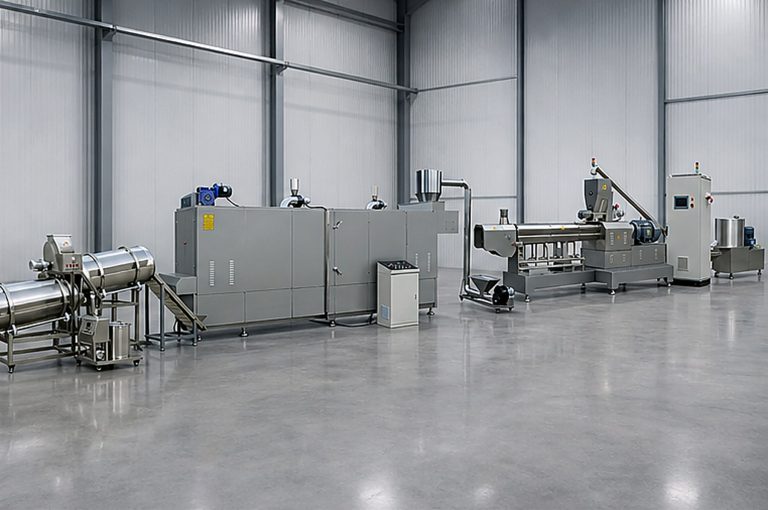
The key point is process ownership. If a buyer is planning fried pellets, the forming, drying and frying stages must be specified as one system. If a buyer is planning directly expanded snacks, the extruder, die, cutter, pneumatic conveying, oven and seasoning stages must be balanced as one system. A supplier cannot decide that boundary reliably from hourly capacity alone.
Use the formulation to test the machine choice
Ask the process team to describe the formula before discussing a model number. The useful inputs are the main starch sources, protein level, fat and sugar additions, moisture before extrusion, required texture and allowed variation between batches. These factors affect material flow, mechanical energy, die pressure, expansion and the downstream drying load.
Research on food extrusion consistently identifies moisture, temperature, screw configuration, feed rate and die design as material process variables, not independent machine settings. A formula with higher protein or lower starch can behave very differently from a simple cereal-rich puff, even at the same nominal throughput. The quotation should therefore state the product basis for capacity and not present one output figure as a universal guarantee.
Capacity is a line calculation, not an extruder label
Compare capacity on the same accepted-product basis. The meaningful question is: how many kilograms of saleable, packed product per hour can the complete line produce under the agreed formula and quality standard?
The extruder may be the process core, but the oven or dryer often sets the sustainable rate. Water removed in drying, residence time, belt loading, seasoning pickup, cooling and packaging handover can all limit output. A line that claims a large extruder capacity but has an undersized dryer will not deliver the same accepted output for long runs.
For a practical comparison, request four figures from each supplier:
- Extruder feed rate and product basis.
- Expected product moisture at the extruder outlet and at packing.
- Dryer duty, residence time and operating condition behind the stated capacity.
- Acceptance capacity after rejects, cooling and packing handover.
For a deeper discussion of this balance, see our guide to matching extruder and oven capacity.
Questions to ask before accepting a proposal
- Does the reference product expand at the die, or later during frying?
- Which raw materials and approximate formula will be used for the acceptance test?
- What product shape, unit weight, density and moisture range are required?
- What is the target rate of accepted finished product, not just extruder output?
- How many molds, shapes or recipes must the line accommodate?
- Which utilities are available: electrical supply, steam, gas, compressed air, water and exhaust capacity?
- Which downstream equipment is included in the stated scope: drying, seasoning, cooling, packing handover and controls?
- What will be demonstrated during the factory acceptance test?
How to structure a useful factory acceptance test
A factory acceptance test should prove an agreed process, not simply show that the machine runs. Bring or agree the product formula and define measurable acceptance points: stable running time, accepted output, product appearance, bulk density or expansion, moisture at the agreed stage, safety checks, utility requirements and the list of unresolved actions.
For a twin-screw project, ask to observe feeding, conditioning, extrusion, die and cutter operation, conveying, drying and seasoning as a connected system. For a single-screw pellet route, include the downstream drying and frying conditions that create the final texture. Our food production line FAT checklist can be used to prepare this conversation before shipment.
A practical decision table
| Project condition | What to evaluate first | Likely direction |
|---|---|---|
| Directly expanded cereal snack | Formula flexibility, die expansion, cutting and drying balance | Twin-screw process is commonly evaluated first |
| Dense pellet expanded later by frying | Forming, pellet drying and frying route | Single-screw forming may be appropriate |
| Several shapes or recurring formula changes | Mixing, moisture control, screw and die changeover | Twin-screw flexibility becomes more valuable |
| One established formula with controlled raw materials | Stable conveying, total line cost and operating simplicity | Evaluate whether a simpler process meets the specification |
| Quoted capacity is the main comparison point | Accepted output after drying, seasoning and cooling | Do not select either machine until the whole line is balanced |
Information to send for a technical proposal
Send product photos or samples, raw-material details, target capacity, process preference, factory dimensions, available utilities, target market and the preferred boundary of supply. State whether the request is for a stand-alone extruder or a complete line. If product details are still being developed, list the assumptions openly so suppliers can distinguish a preliminary proposal from a guaranteed process specification.
For directly expanded snacks, start with our puffed snack production line process guide. For a project discussion, send the available information through the ZEKO contact page and we can help define the process route before a final configuration is chosen.
Technical references
- Review of extrusion effects on starch structure and digestibility, including a summary of single- and twin-screw food extruder principles.
- ENERGY STAR breakfast cereal production guide, which discusses mixing and cost considerations for cereal extrusion.
- Quantitative modeling perspective on aquafeed and pet food extrusion, for the interaction of formulation, energy input and processing conditions.
Continue Reading